How Medo Conducts Rigorous Quality Control for Insulated Bottles
At Medo Drinkware, ensuring every insulated bottle meets the highest standards is a core part of our manufacturing philosophy. Our quality control (QC) process is integrated at every stage of production, from raw materials to the finished product. Here’s an inside look at how we guarantee the durability, safety, and performance of our bottles.
1. Incoming Raw Material Inspection
Quality begins with the materials. We source high-grade 304/316 stainless steel, food-grade silicone, and BPA-free plastics. Each batch of incoming materials undergoes strict inspection for:
- Material Certification: Verification of mill test certificates for stainless steel composition.
- Dimensional Checks: Ensuring thickness and specifications match our design requirements.
- Surface Quality: Inspecting for scratches, dents, or impurities.
2. In-Process Production Checks
During manufacturing, our QC team performs checks at critical stages:
- Stamping & Forming: Checking for precise dimensions and structural integrity of bottle bodies and caps.
- Welding (for vacuum insulation): Using helium mass spectrometry to test the integrity of the vacuum seal—a crucial step for thermal performance.
- Polishing & Coating: Visual and tactile inspections for a smooth, even finish without defects.
- Assembly: Ensuring threads align correctly, lids seal properly, and components like straws or flip lids function smoothly.
3. Performance and Safety Testing
Finished bottles are subjected to a battery of tests:
- Thermal Retention Test: Bottles are filled with hot or cold water and monitored over 12-24 hours to verify insulation meets claimed standards (e.g., keeping liquids hot for 12+ hours).
- Leak Test: Each bottle is pressurized and submerged to check for any air or liquid leakage.
- Drop Test: Samples are dropped from specified heights onto hard surfaces to assess durability and impact resistance.
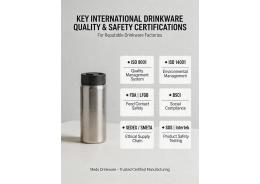
- Chemical Safety Test: Ensuring no harmful substances migrate into liquids, complying with FDA, LFGB, and other international standards.
4. Final Random Inspection (FRI)
Before packaging, a random sample from each production batch undergoes a final audit. This includes:
- Re-checking appearance, color, and print quality.
- Verifying all components are present and functional.
- Confirming packaging and labeling accuracy.
Only after passing all these stringent checks does a Medo insulated bottle earn its place in your hands. Our commitment to quality ensures you receive a reliable, safe, and high-performing product for your daily hydration needs.
Explore our collection of rigorously tested insulated bottles at Medo Drinkware.
 English
 German
 French
 Russian
 Spanish
 Japanese
 Korean
 Portuguese
 Ukrainian
 Arabic
 Italian